Short answer
The decision rule
Size a printer farm from good-parts demand, cycle time, first-pass yield, planned availability, operator touch time and post-processing capacity. Start with a pilot cell, record the assumptions and expand only after the agreed output, alert handling, maintenance and repeatability gates are met.
01
Translate demand into a capacity model
Start with part families, monthly demand, build time, yield, setup, changeover and post-processing. Printer count is the output of that model, not the starting assumption. Include peak demand and a realistic utilization target rather than planning every machine at one hundred percent.
A pilot cell provides real data for loading, failure rates, operator attention and finishing time. Use that evidence to decide when and how to add the next block of capacity.
02
Design operator flow before choosing racks
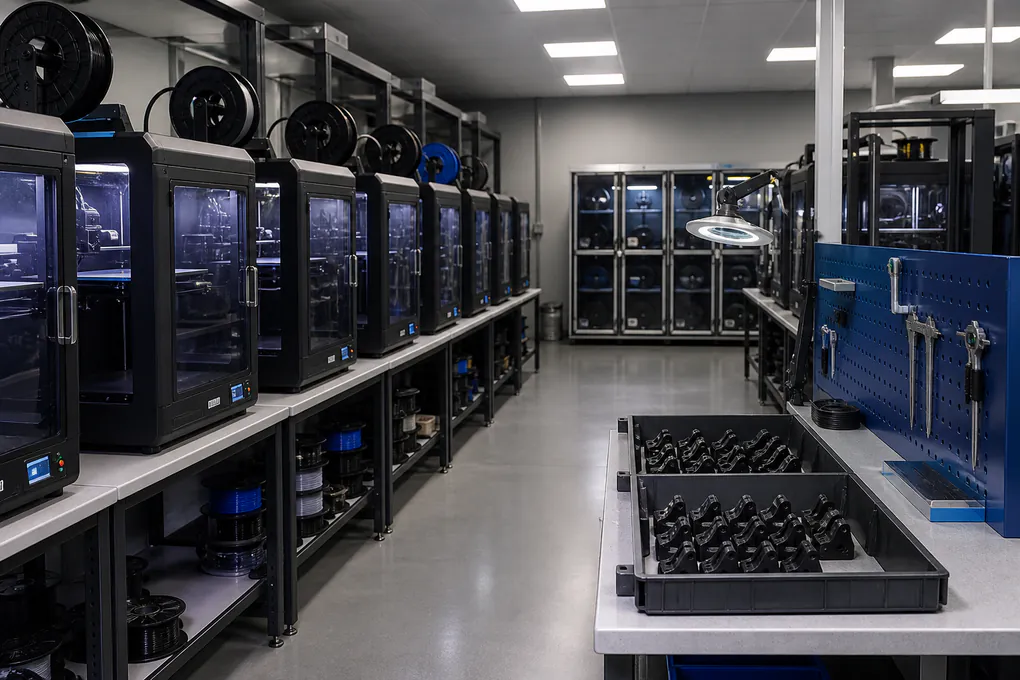
Map material receiving, drying, job preparation, printer loading, part removal, inspection, rework, packing and waste. The layout should reduce unnecessary movement while preserving safe access, ventilation and maintenance clearance.
Standard work at each station improves repeatability. Visual status, defined work-in-progress locations and clear ownership prevent a large fleet from becoming a collection of individual hobby workflows.
03
Standardize the production platform
Too many printer, nozzle, firmware and material combinations increase training, spare parts and troubleshooting complexity. Standardize where possible, then document the approved exceptions required for specific part families.
- Approved printer and firmware versions
- Controlled profiles by material and part family
- Scheduled preventive maintenance
- Minimum spare-unit and critical-parts stock
- Change-control record for process updates
04
Measure the metrics that drive reliable output
Track good parts per operator hour, first-pass yield, material loss, labor per job, queue time, reprint causes and downtime. Utilization alone can reward machines that stay busy producing low-value or failed work.
A simple daily review of constraints and failure categories often produces more value than an elaborate dashboard with inconsistent data. Improve the bottleneck that limits accepted good parts.
05
Build supply resilience into the farm
Forecast materials and critical spares with lead times and demand variability. Qualify alternatives before a shortage, and keep a controlled process for material or component substitutions.
Project planning should cover phased rollout, replacement units, spare-parts availability and service escalation. A scalable farm is a supply system as much as a bank of machines.
Working tool
Calculate printer count from accepted-part demand
For a homogeneous job family, N = ceiling(D × t / (H × A × B × Y)). D is accepted-part demand per month; t is machine occupancy hours per build, including setup/removal; H is scheduled hours per printer per month; A is the available fraction of scheduled time; B is parts started per build; Y is the accepted fraction. Use fractions between 0 and 1 for A and Y. Avoid subtracting the same downtime in both t and A.
Teaching example, not measured EverBen output: D = 1,200 parts/month, t = 4 hours/build, H = 160 hours/month, A = 0.80, B = 4 parts/build and Y = 0.90. One printer provides 160 × 0.80 / 4 × 4 × 0.90 = 115.2 expected accepted parts/month. N = ceiling(1,200 / 115.2) = 11 printers. At A = 0.65 the estimate becomes 13 printers. Round to whole builds when scheduling; expected yield is a planning average.
| Input to measure | Record during the pilot |
|---|---|
| Build occupancy and loading | Hours from loading/setup until the printer is available for the next job; parts started per build. |
| Availability and yield | Scheduled hours, unavailable hours with causes, started parts and accepted parts. |
| Mixed part families | Calculate required machine hours for each family and add them; account for changeover and due-date constraints. |
Working tool
Check labor and finishing before adding printers
The printer calculation is one capacity limit. Separately compare loading labor, finishing, inspection and packing with their staffed capacity. The station with the lowest accepted output limits the cell. Do not multiply a finished-part yield into the model twice.
For the same teaching example, 1,200 / (4 × 0.90) requires about 334 builds per month. At an assumed 0.25 operator hour per build, loading and unloading need 83.5 operator hours before finishing, inspection or maintenance. If finishing can release only 1,000 accepted parts per month, eleven printers cannot achieve a 1,200-part delivery target without more finishing capacity.
| Daily record | Use in the decision |
|---|---|
| Scheduled / unavailable hours and cause | Review availability assumptions and recurring stoppages. |
| Builds, started parts and accepted parts | Check occupancy time and accepted yield by part family. |
| Operator touch time and station queues | Find labor and finishing constraints before buying capacity. |
Sources
Primary references and source-check scope
The original references were checked on 2026-09-02; any later reference check is identified below. The live issuing body remains the source of truth. A standards record does not replace the full standard or professional judgment.
ISO: ISO/ASTM 52920:2023 — Qualification principles for industrial AM processes and production sites
Official standard record for production-process and site quality-assurance considerations.
Open the official source →NIST: Additive Manufacturing
Public technical program covering AM measurement science, process understanding and qualification.
Open the official source →Revision, authorship and corrections
Updated 2026-09-08: added the comparison/calculation tools and a blank worksheet above. The organization byline identifies the publisher; no individual author credentials, named technical reviewer or professional approval is asserted. Read the source and correction notes.
Send factual corrections to 3dprint@oem3dprinter.com with the article URL, passage and supporting source. Use current project documents and competent review for safety-critical or regulated decisions.