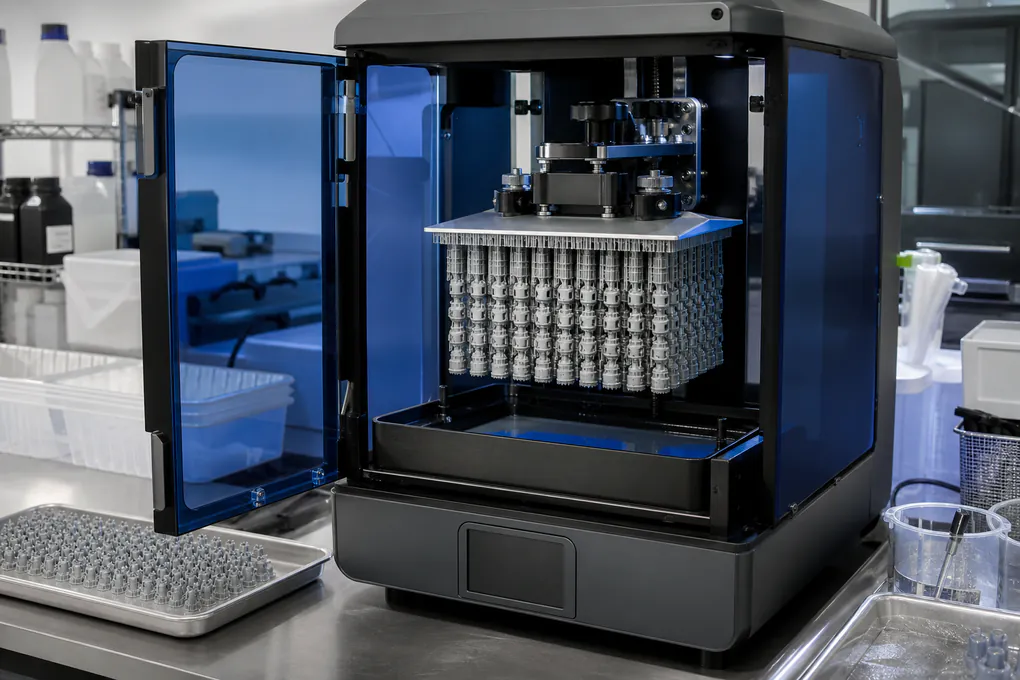
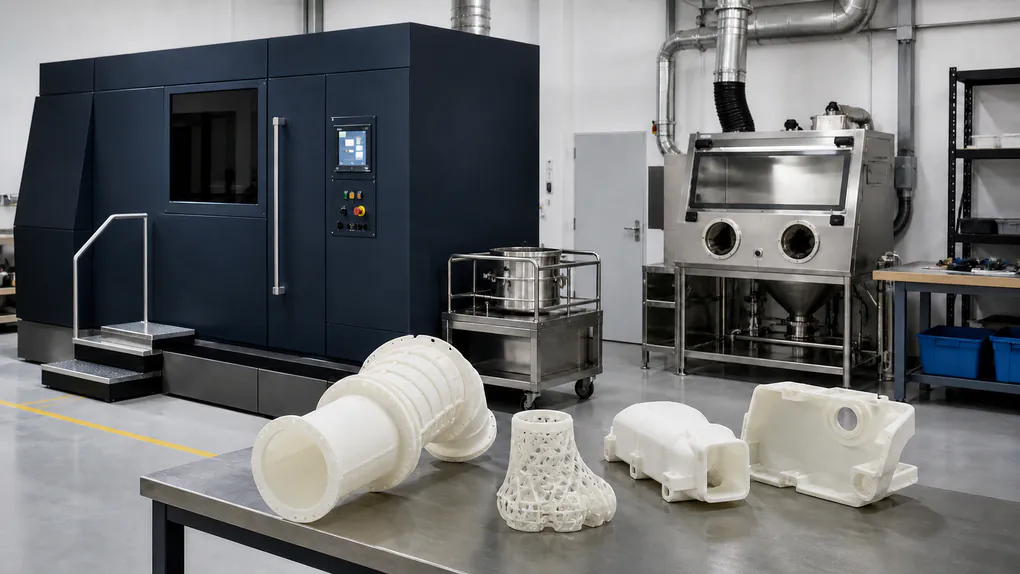
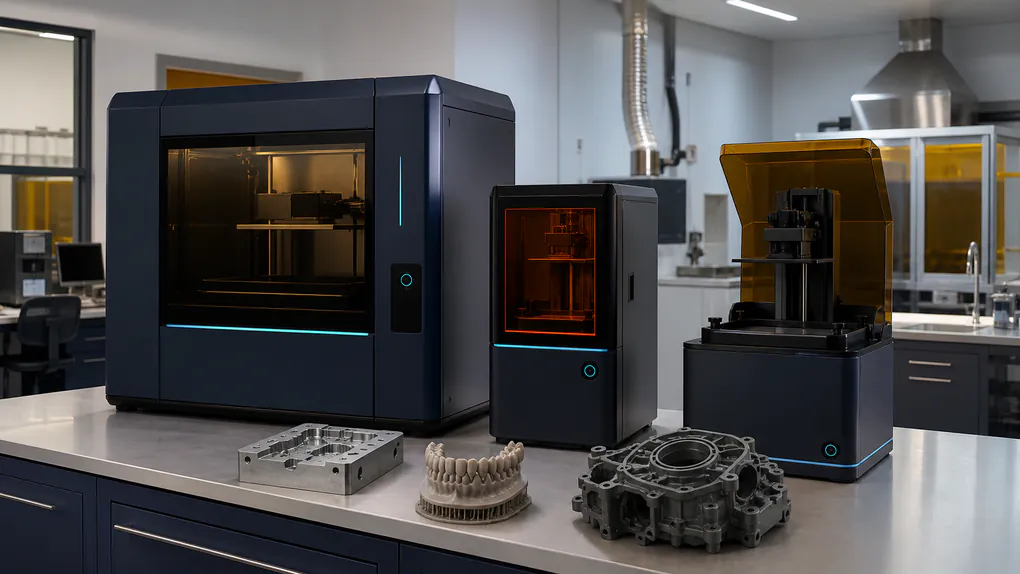
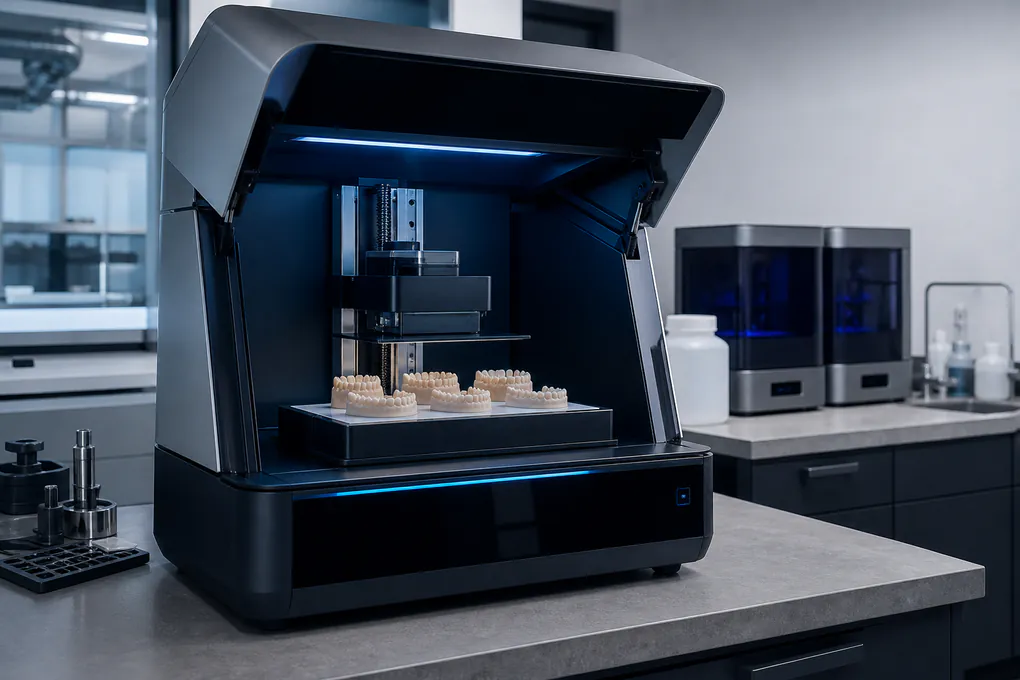
Unbranded industrial SLA resin 3D printer systems in a clean additive manufacturing lab

SLA resin systems · OEM & bulk procurement

Industrial SLA 3D Printers specified around your production requirement

Custom and bulk-purchase SLA platforms for large prototypes, masters, patterns and production tooling—with laser, resin, sample and acceptance requirements defined before quotation.

Illustrative technology image. The final proposal names the actual model, revision, production site and configuration.

Buyer painQuotes that cannot be compared because model scope, evidence and site work are different.
EverBen approachOne requirement brief, one return-field table and written acceptance gates.
Commercial modelMOQ, OEM program and bulk pricing are provided for the approved configuration.

EverBen equipment directory

12 EverBen models and series in this process family

Compare model summaries, configuration limits and adjacent models. Each detail page identifies its reference status and separates pending fields from reference values.

Current availability and the mapping to a quoted machine are pending confirmation for every record. Source specifications require a current signed datasheet; conflicting fields remain open.

SLA · Model

EverBen SLA 850 Pro 3D Printer

SLA 850 Pro: 850 × 850 × 500 mm resin build reference in the same listed machine outline as SLA 800. The first tank rises to 527 kg; cost and output advantages need a shared trial.

Build envelope
850 × 850 × 500 mm
Layer setting
0.05 – 0.2 mm
Laser
Solid-state frequency-tripled Nd:YVO₄

Availability: pending confirmation · Needs configuration confirmation
SLA · Model

EverBen SLA 400 Pro 3D Printer

SLA 400 Pro: 400 × 400 mm SLA platform reference with 200 or 300 mm height options and an explicit 355 nm wavelength. Build height, resin fill and electrical phase need pairing.

Build envelope
400*400*200mm / 400*400*300mm
Layer setting
Optional (between 0.05mm-0.2mm)
Laser
Diode-Pumped Solid-State Laser Nd, Wavelength 355nm

Availability: pending confirmation · Needs configuration confirmation
SLA · Model

EverBen SLA 650 Pro 3D Printer

SLA 650 Pro: SLA 650 has an unresolved build-size unit conflict. The table records 255 kg first-tank resin and 1000 kg machine mass; verify the envelope before comparing it with SLA 600.

Build envelope
Pending confirmation — Source records conflict on dimensions and units; confirm the usable X/Y/Z envelope for the quoted revision.
Layer setting
0.05mm~0.2mm
Laser
Solid-state frequency tripled Nd: YVO4

Availability: pending confirmation · Needs configuration confirmation
Owner-supplied third-party catalog reference

Industrial SLA 3D Printers attributes to confirm in the named proposal

These ranges come from a third-party 2025 equipment catalog supplied by the site owner. They are not EverBen-branded specifications and do not prove manufacturing, authorization or current availability. A named manufacturer, authorization status and current signed datasheet must control any proposal or order.

ProcessScanning-laser vat photopolymerization
Catalog reference build range400 × 400 × 200/300 mm to 2700 × 900 × 800 mm; exact model confirmation required
Catalog light source355 nm laser architecture; exact source and installed power to be confirmed
Catalog layer modesCommon reference modes include 0.05 / 0.10 / 0.15 mm; material and geometry dependent
Industrial options to scopeSingle, dual or triple scan-head layouts; resin handling, heating and quick-release recoater by configuration
Buyer acceptance focusLarge-part distortion, seam or zone consistency, surface finish, repeatability and resin lot control

01 · Application fit · SLA resin

When Industrial SLA 3D Printers is the right process—and when another route is safer

SLA scans a focused ultraviolet laser across a liquid photopolymer vat, then changes the build height and repeats the exposure layer by layer.

The strongest starting cases for this SLA resin review are large appearance prototypes, master patterns and casting patterns, automotive verification parts, tooling and composite lay-up aids. The intended output must still be separated into prototype, tooling, bridge production or released production because the evidence and responsibility change at each stage.

SLA resin go/no-go question

Can the proposed process meet the part duty, material route and acceptance method for large appearance prototypes without relying on an unverified brochure claim?

02 · Machine architecture · SLA resin

Industrial SLA 3D Printers architecture that changes the buying decision

Large-format SLA configurations can differ in scan-head count, optical calibration, recoating, vat control, platform handling and resin temperature management.

The proposal must name the installed configuration and explain how it supports large appearance prototypes. The process label is not enough when the build mechanism, thermal or optical design, feed system and accessories can change both performance and maintenance.

SLA resin configuration freeze

For the proposed SLA resin route, record the manufacturer, model, revision, installed options, cell boundary and every third-party dependency before quotations are compared.

03 · Build and footprint · SLA resin

Industrial SLA 3D Printers build envelope, part orientation and factory access

The owner-supplied catalog reference lists 400 × 400 × 200/300 mm to 2700 × 900 × 800 mm; exact model confirmation required. Treat that only as an early planning range until the authorized manufacturer returns a current model and signed datasheet.

For master patterns and casting patterns, usable space depends on orientation, process margins, unloading and downstream handling. The site review must also cover machine footprint, packed size, weight, doorway route, floor loading and service clearance.

SLA resin space validation

Fit a representative master patterns and casting patterns part in the usable SLA resin envelope, then verify unloading, service access, packed dimensions and floor load for the named machine.

Have the part file or target specification?Send non-confidential inputs now; attach controlled files only after the project route is confirmed.
Open RFQ form

04 · Material route · SLA resin

Industrial SLA 3D Printers materials, conditioning and lot evidence

Industrial SLA routes may use general modelling, tough, high-temperature, casting, transparent or application-specific photopolymers.

The material brief should connect the exact grade or SKU with storage, conditioning, the proposed SLA resin configuration, process parameters, post-processing and the property test method. Bulk or private-label discussions begin only after this compatibility route is defined.

SLA resin material qualification

Approve one traceable SLA resin grade or SKU with its TDS, SDS, lot evidence, conditioning, parameter revision and downstream process.

05 · Part quality · SLA resin

Industrial SLA 3D Printers accuracy, repeatability and the real error mechanisms

Large SLA parts are especially sensitive to resin shrinkage, support layout, scan-zone calibration, recoating and post-cure restraint.

Use a representative automotive verification parts geometry or an agreed coupon. Record orientation, material lot, build position, post-process, datum scheme, instrument and repeat count so input resolution cannot be mistaken for verified finished-part capability.

SLA resin measurement evidence

Use the same automotive verification parts geometry, material, orientation, post-process, datums, instrument and repeat count for every SLA resin candidate.

06 · Output and TCO · SLA resin

Industrial SLA 3D Printers throughput measured as accepted parts

Layer area, scan path, recoating time, support volume, drain time and post-cure capacity determine output more reliably than peak scan speed.

A purchasing model for SLA resin should count preparation, changeover, build, cooling or curing, recovery, finishing, inspection, rejected parts and maintenance. Compare good parts per staffed shift and the consumables that control uptime rather than one peak speed value.

SLA resin capacity basis

Calculate accepted SLA resin parts per staffed shift with stated yield, changeover, downstream capacity, maintenance and consumable-life assumptions.

Have the part file or target specification?Send non-confidential inputs now; attach controlled files only after the project route is confirmed.
Open RFQ form

07 · Digital workflow · SLA resin

Industrial SLA 3D Printers software, parameter access and production data

The workflow may include repair, orientation, support generation, slicing, laser-path planning, nesting and multi-machine job transfer.

For a controlled large appearance prototypes workflow, ask about file preparation, profile revision, user roles, offline operation, job records, export, backup, licences and remote support. OEM interface or MES work needs a separate functional specification and acceptance test.

SLA resin data-rights check

For Industrial SLA 3D Printers, freeze licence term, parameter access, offline rights, job-record export, backup, update policy and the remote-service security boundary.

08 · Site and EHS · SLA resin

Industrial SLA 3D Printers utilities, operator exposure and safety boundary

Plan electrical supply, stable room temperature and humidity, resin storage, ventilation, cleaning liquids, UV-safe handling and floor loading.

The site-readiness return should assign every SLA resin utility, material-control and safety task to the buyer, equipment supplier or a licensed local contractor. A generic certificate cannot replace the exact declaration, manual, interlock review and destination-specific risk assessment.

SLA resin site-readiness gate

Approve the SLA resin utilities, extraction, material storage, fire controls, PPE, access and contractor responsibilities before shipment release.

09 · Downstream process · SLA resin

Industrial SLA 3D Printers post-processing and inspection capacity

Typical steps are draining, support removal, washing, secondary UV cure, sanding, sealing or painting, plus dimensional inspection.

Size the downstream route for the planned tooling and composite lay-up aids load. Identify included equipment, buyer-supplied tools, subcontracted operations, consumables, waste streams and the quality gate that releases the finished part.

SLA resin downstream capacity

Confirm every SLA resin finishing and inspection step, its owner, batch capacity, consumables, waste route and release record.

Have the part file or target specification?Send non-confidential inputs now; attach controlled files only after the project route is confirmed.
Open RFQ form

10 · Technical acceptance · SLA resin

Industrial SLA 3D Printers sample build, FAT and SAT evidence

Use a full-scale risk section or representative large geometry to expose warp, surface, zone matching and support-removal issues.

The SLA resin acceptance document should fix the sample, material, configuration, parameters, inspection, pass criteria, witness method and corrective-action route. FAT verifies the contracted system before shipment; SAT closes installation and agreed output at the buyer site.

SLA resin acceptance record

Do not authorize the SLA resin shipment or final handover until the named configuration passes the agreed sample, inspection and corrective-action method.

11 · Project deployment · SLA resin

Industrial SLA 3D Printers installation, training and production handover

Deployment for SLA resin should start with the site drawing, access route, readiness checklist, shipment condition and named contacts. Commissioning records must connect utilities, safety checks, calibration, software setup and the acceptance build.

Operator training should use the proposed Industrial SLA 3D Printers workflow and cover material handling, job preparation, routine maintenance, fault recovery and quality records. Manuals, language, attendees, practical exercises and competency sign-off belong in the quote.

SLA resin handover package

Close Industrial SLA 3D Printers commissioning with signed readiness, calibration, sample, training, manuals, maintenance, spares and escalation records.

12 · Lifecycle and OEM scope · SLA resin

Industrial SLA 3D Printers warranty, spares, authorization and project terms

SLA lifecycle planning should include vats or recoaters, filters, optical service, resin contamination control, calibration and cleaning consumables.

Review machine colour, nameplate, interface language, documentation, accessories and selected mechanical or workflow options against MOQ and engineering effort. The response must also identify the authorized manufacturer and seller, MOQ, forecast, packing, delivery term, warranty start, exclusions, labour or travel treatment, critical spares and change-notification policy. No retail price can represent those variables safely.

SLA resin commercial boundary

The signed SLA resin offer must identify authorization, MOQ, OEM scope, delivery, warranty, exclusions, service responsibility, critical spares and change control.

Your RFQ inputs

What a Industrial SLA 3D Printers buyer should send

  • Largest part file and preferred orientation
  • Surface, tolerance and dimensional inspection requirements
  • Resin property and downstream finishing needs
  • Monthly build mix and target delivery window
  • Site voltage, access, temperature and humidity

Comparable supplier return

What the sla resin systems response should answer

  • Named build envelope and laser/scan-head configuration
  • Representative sample plan with measurement method
  • Approved resin list and material-management scope
  • Machine, accessory, software and post-process boundary
  • FAT, installation, training, warranty and spares plan

B2B procurement FAQ

Industrial SLA 3D Printers questions before technical shortlisting

Is a larger SLA build volume automatically better?

No. Choose the smallest usable envelope that fits orientation, supports and handling, then confirm distortion, scan-zone consistency and post-cure capacity.

Can private-label SLA equipment be requested?

Yes as an inquiry requirement, but feasibility must be confirmed by the authorized manufacturer after the target model, annual volume, destination and validation scope are defined.

What file should I send for a sample?

A non-confidential STL or STEP file plus critical dimensions, surface expectations, resin properties and inspection method is the best start.

How should SLA accuracy be compared?

Compare measured parts made in the intended resin, orientation and post-cure route. Laser spot and layer height alone are not finished-part accuracy.

Next practical step

Build a comparable RFQ for industrial sla 3d printers.

Send the part, material, output, destination and acceptance target. The inquiry process structures the configuration, open questions and validation route without publishing a misleading retail price.

Request a custom B2B quote