Short answer
The decision rule
Audit the complete LPBF cell: machine, powder lifecycle, atmosphere, filtration, parameters, software, utilities, post-processing, inspection and support. Ask for named-model evidence and test conditions. A brochure range or one best sample cannot establish repeatable production capability.
01
Audit the process chain, not only the machine
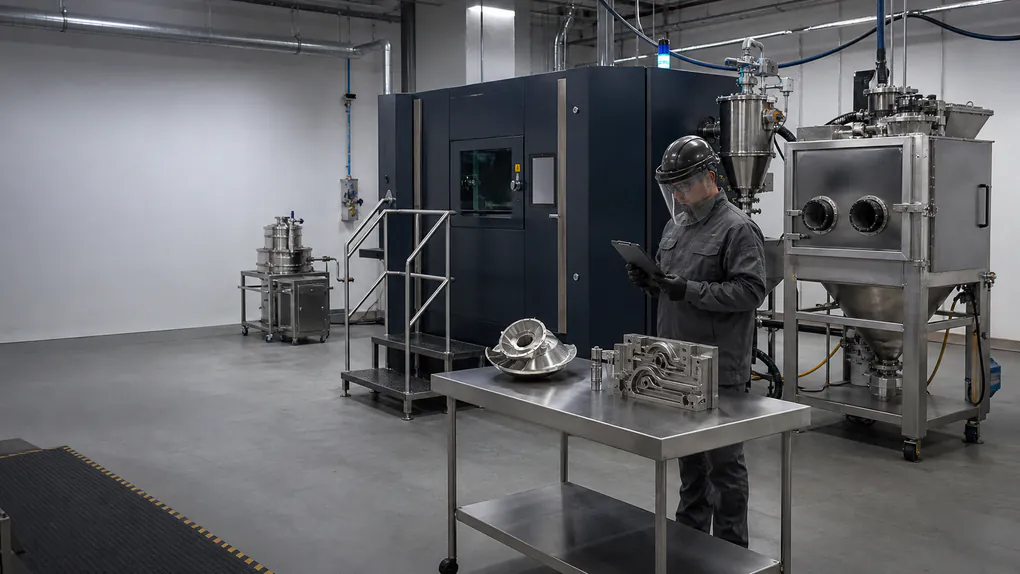
Metal additive performance depends on equipment, powder condition, parameter control, atmosphere, part preparation, heat treatment, support removal, finishing and inspection. A supplier audit should trace how those elements are controlled together.
Ask which responsibilities are covered in the proposed project scope and which require partners or additional equipment. This prevents a narrow machine comparison from hiding major cell-level capability gaps.
02
Review objective build evidence
Request reports that connect material, parameter set, density, mechanical properties, dimensional capability and surface condition. Evidence should identify the machine configuration and test method. Results from another laser count, chamber size or material route may not transfer directly.
- Density and metallography records
- Tensile results with build orientation
- Dimensional coupon data across the plate
- Oxygen trend and gas-consumption data
- Repeatability across more than one build
03
Treat powder handling as a core system
Powder receiving, storage, sieving, recycling, transfer, exposure control and waste management must be designed before installation. Review compatible alloys, inerting strategy, grounding, housekeeping, operator protection and local regulatory requirements with competent safety professionals.
A closed or semi-closed route can reduce handling but does not remove the need for training, monitoring and documented procedures. Site readiness should be confirmed before the machine ships.
04
Define acceptance before technical route approval
A factory acceptance test and site acceptance test should state the sample geometry, material, build conditions, measurements, pass criteria, responsibilities and remedy if criteria are not met. Ambiguous acceptance language creates disputes after delivery.
Include software licenses, parameter access, utilities, installation, calibration, training, spare parts and the support escalation path. The acceptance document is often more valuable than another marketing comparison table.
05
Model five-year operating reality
Compare gas, filters, recoater elements, optics, service, software, powder loss, labor, heat treatment, finishing and quality assurance. Consider expected utilization and the cost of downtime under your service arrangement.
A technically suitable machine with responsive regional support can be a better investment than a faster specification with uncertain service coverage. Procurement should balance performance, evidence, safety and lifecycle support.
Working tool
Use an evidence and action register during the audit
Copy the checks below into an audit record. For each item enter the exact evidence identifier and revision, finding, responsible person, due date and closure decision. A received document remains under review until its identity and scope have been checked. This is a blank buyer worksheet, not a report of an EverBen factory audit.
| Audit item | Evidence to examine |
|---|---|
| Supplier and site | Registered entity, manufacturer relationship, site identity and scope of the proposed production work. |
| Quoted configuration | Model, serial or build identifier, laser/options list, software and approved configuration revision. |
| Powder and process | Alloy/lot record, reuse history, parameter revision, atmosphere log and change controls. |
| Test build | Build file, coupon locations/orientations, post-processing, instruments, reports and repeated results. |
| Cell and operators | Site review, powder-handling arrangements, training records and assigned safety responsibilities. |
| Acceptance and service | FAT/SAT criteria, deviations, release authority, support provider and compatible spares. |
For a non-applicable check, record the reason and approving reviewer. A missing record is an open action, not a passing result.
Working tool
Calculate five-year cost on one production-cell boundary
Undiscounted five-year cost = equipment and auxiliaries + installation and qualification + total operating costs over years 1–5 − residual value. Operating costs include material loss, gas, energy, filters, wear parts, labor, software, maintenance, external finishing/inspection and downtime costs. Count each cost once; state currency, taxes, financing, inflation and any omitted categories.
Teaching example in arbitrary currency units: 100,000 for equipment/auxiliaries + 20,000 for installation/qualification + 5 × 30,000 annual operating cost − 10,000 residual value = 260,000 over five years. At 25,000 accepted parts over that period, cost is 10.40 per accepted part. These assumed inputs are not EverBen prices, forecasts or measured economics.
| Input | Evidence to use in your calculation |
|---|---|
| Initial cost | Quoted machine, peripherals, installation, qualification and site works within the agreed boundary. |
| Annual operating cost | Pilot consumption and labor, maintenance plan, vendor quotations and externally performed operations. |
| Accepted output / residual value | Demand and yield scenarios with a stated utilization basis; document the residual-value assumption. |
Compare low, base and high utilization cases. If a present-value comparison is required, apply the same discount rate and timing convention to every alternative.
Sources
Primary references and source-check scope
The original references were checked on 2026-09-02; any later reference check is identified below. The live issuing body remains the source of truth. A standards record does not replace the full standard or professional judgment.
ISO: ISO/ASTM 52920:2023 — Qualification principles for industrial AM processes and production sites
Official standard record for quality-assurance factors at AM production sites.
Open the official source →ISO: ISO/ASTM 52928:2024 — Metal powder life cycle management
Official standard record for powder properties, testing and lifecycle controls.
Open the official source →NIST: Additive Manufacturing Powder Metrology Laboratory
Public technical reference for powder flowability, spreadability, particle size and powder-layer measurements.
Open the official source →OSHA: Combustible Dust Technical Manual
Official safety reference explaining why fine-powder hazards require site-specific professional review.
Open the official source →Revision, authorship and corrections
Updated 2026-09-08: added the comparison/calculation tools and a blank worksheet above. The organization byline identifies the publisher; no individual author credentials, named technical reviewer or professional approval is asserted. Read the source and correction notes.
Send factual corrections to 3dprint@oem3dprinter.com with the article URL, passage and supporting source. Use current project documents and competent review for safety-critical or regulated decisions.